
In an era defined by rapid technological advancement, from microelectronics to sustainable energy solutions, the foundational role of seemingly simple chemical compounds often goes unnoticed. Yet, behind every sleek gadget, every efficient manufacturing process, and every step towards a greener future, complex chemical interactions are at play. Among these essential building blocks is sodium metabisulfite (SMBS), a versatile inorganic salt whose applications, while diverse, hold particular significance within the sprawling landscape of modern technology. Far from a mere laboratory curiosity, SMBS functions as a critical enabler across various high-tech industries, influencing everything from the purity of materials to the sustainability of production cycles. Understanding this compound is not just about comprehending its chemical formula, but appreciating its subtle yet profound impact on the technological innovations that shape our world.

Unveiling Sodium Metabisulfite: A Fundamental Chemical Compound
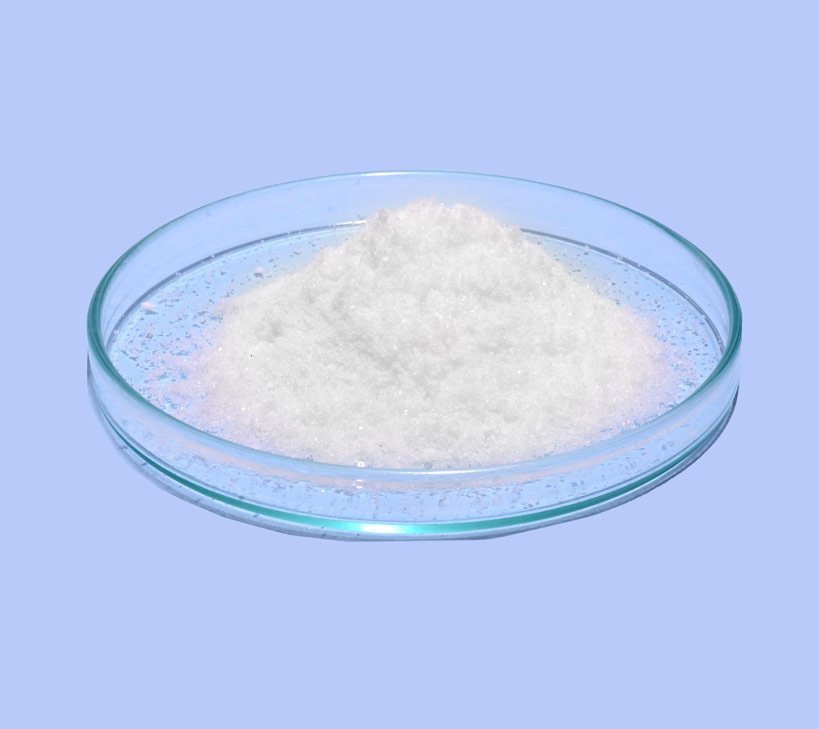
Sodium metabisulfite, chemically represented as Na2S2O5, is a white or yellowish-white crystalline powder with a characteristic sulfur dioxide odor. It is a highly soluble compound that plays a significant role in various industrial applications due to its potent reducing and antioxidant properties. While its primary identity is that of a chemical compound, its fundamental characteristics and the infrastructure around its production are deeply interwoven with technological progress.
The Basics: Chemical Structure and Properties
At its core, sodium metabisulfite is a salt formed from sodium ions (Na+) and the metabisulfite ion (S2O5^2-). When dissolved in water, it readily dissociates and releases sulfur dioxide (SO2), a gas known for its reducing and antimicrobial properties. This ability to generate SO2 in situ is what makes SMBS so valuable. Its strong reducing capacity means it can donate electrons to other substances, preventing oxidation or breaking down unwanted compounds. This is particularly crucial in tech sectors where material integrity and process control are paramount. For instance, preventing oxidation can extend the lifespan of electronic components or preserve the quality of raw materials used in advanced manufacturing.
Furthermore, its acidity, typically around a pH of 4.0 when dissolved, contributes to its efficacy in various applications, from acting as a bleaching agent to a disinfectant. The stability of SMBS in its solid form, coupled with its ready reactivity in aqueous solutions, makes it an ideal chemical for industrial-scale operations that demand precise control and consistent performance. Its physical and chemical properties, therefore, are not just academic points but functional attributes that enable specific technological outcomes, from processing rare earth metals to preparing circuit boards.
Industrial Synthesis and Supply Chains
The production of sodium metabisulfite itself is a testament to industrial chemical engineering. It is typically synthesized by reacting sulfur dioxide gas with sodium carbonate or sodium hydroxide solutions. The subsequent crystallization and drying processes are engineered for efficiency, purity, and scalability, reflecting advanced chemical manufacturing technologies. The global supply chain for SMBS is robust, driven by demand from diverse sectors, many of which are integral to the tech economy. These supply chains are increasingly optimized through digital logistics, AI-driven demand forecasting, and sophisticated tracking systems – all technologies that indirectly rely on such fundamental chemicals.
Ensuring the purity of industrial-grade SMBS is critical, as contaminants could compromise sensitive tech manufacturing processes. Companies that produce SMBS invest heavily in quality control technologies, using advanced analytical instruments and statistical process control to meet stringent specifications. This meticulous approach to production underscores how even a seemingly common chemical is produced using and for, high-tech standards, illustrating a symbiotic relationship between chemical manufacturing and broader technological advancements.
Essential Roles in Manufacturing and Material Science
The technological landscape is built upon a foundation of meticulously engineered materials and precisely controlled manufacturing processes. In numerous instances, sodium metabisulfite acts as a silent but indispensable enabler, contributing to the quality, integrity, and efficiency of these critical operations.
Safeguarding Industrial Processes: Preservative and Antioxidant Functions
In the realm of high-tech manufacturing, particularly where sensitive materials are involved, oxidation can be a formidable enemy. Exposure to oxygen can degrade polymers, corrode metals, or alter the properties of semiconductor materials, leading to product failure or reduced performance. Sodium metabisulfite, with its potent antioxidant properties, is employed to mitigate these risks. It acts as a sacrificial reducing agent, reacting with oxygen or other oxidizing agents before they can harm more valuable components.
For example, in the production of certain specialized plastics and resins used in electronics casings, optical components, or aerospace applications, SMBS can be added during processing to prevent premature degradation. Similarly, in the storage and transport of certain industrial chemicals that are precursors for advanced materials, SMBS ensures their stability and purity, safeguarding expensive raw materials and preventing costly downtime in subsequent manufacturing stages. Its role here is preventive maintenance at a chemical level, a foundational aspect of ensuring operational reliability in tech-intensive industries.
The Reducing Agent: From Photography to Polymers
The reducing power of SMBS finds diverse applications that indirectly or directly contribute to technological output. Historically, it was a crucial component in photographic developing solutions, where it acted as a preservative for the developer, preventing its oxidation by air. While traditional photography has evolved, the principles of chemical processing for imaging and microfabrication persist.
In modern applications, SMBS is used as a reducing agent in various chemical synthesis pathways. It can facilitate the formation of certain polymers that are critical for coatings, adhesives, and composite materials used in industries ranging from automotive tech to renewable energy. For instance, in some polymerization reactions, SMBS helps initiate or control the reaction, ensuring consistent polymer chain lengths and desired material properties. Beyond polymers, it’s utilized in the purification of certain metals and inorganic compounds vital for specialized alloys and catalysts used in high-performance computing, battery technology, and more. This precise chemical control over material properties is a cornerstone of advanced technological development.
Enabling Advanced Materials: Metallurgy and Beyond
The quest for advanced materials with superior strength, conductivity, and thermal resistance is a continuous driver of innovation in technology. Sodium metabisulfite plays a subtle yet significant part in metallurgy and the processing of various inorganic materials. In mining and metal extraction, SMBS can be used in some hydrometallurgical processes to reduce metal ions, aiding in their separation and purification. This is particularly relevant for critical minerals and rare earth elements that are essential components of modern electronics, electric vehicles, and high-performance magnets.
Furthermore, in specialized manufacturing like circuit board etching or surface preparation for plating, SMBS can be used to neutralize excess oxidizing agents or clean surfaces, ensuring optimal adhesion and electrical conductivity. Its application in these contexts ensures the foundational integrity of components that underpin digital communication and data processing. Without such precise chemical interventions, the miniaturization and efficiency of current technological devices would be far more challenging to achieve.
Sodium Metabisulfite in Environmental Technology and Sustainability
As the global focus shifts towards sustainable practices and environmental responsibility, the role of chemicals in mitigating pollution and enabling cleaner technologies becomes paramount. Sodium metabisulfite, paradoxically given its sulfur content, is a key player in various environmental technology applications, particularly those linked to industrial processes.
Water Treatment for High-Tech Industries
Water is a critical resource in virtually all industrial processes, and nowhere is its purity more crucial than in high-tech manufacturing. Semiconductor fabrication, pharmaceutical production for biopharmaceuticals (an emerging tech sector), and specialized chemical synthesis all demand ultra-pure water. Sodium metabisulfite is widely used in wastewater treatment plants, especially in dechlorination processes. Many industrial operations, including those in the tech sector, use chlorinated water for disinfection. Before this water can be discharged back into the environment or reused, the residual chlorine must be removed to prevent ecological harm. SMBS efficiently reduces chlorine into chloride ions, rendering it harmless.
Moreover, in the treatment of specific industrial effluents, SMBS can be used to precipitate heavy metals or reduce certain toxic compounds, making the wastewater safer for discharge. This application is vital for tech companies striving to meet stringent environmental regulations and demonstrate their commitment to sustainable operations. By enabling effective wastewater management, SMBS indirectly supports the “clean” image and operational continuity of technology companies.
Waste Management and Pollution Control
Beyond water treatment, SMBS contributes to broader pollution control strategies. In some industrial emissions, particularly those containing sulfur dioxide (a gas that SMBS can release or react with), SMBS can be used in scrubbing processes. While SMBS itself contains sulfur, its controlled application can be part of a multi-stage process to manage other pollutants. For instance, it can be used in some flue gas desulfurization (FGD) technologies to capture SO2 emissions from industrial boilers and power plants, which might be powering tech manufacturing facilities.
Furthermore, in certain waste recycling processes, SMBS might play a role in breaking down or treating specific contaminants, making subsequent recycling steps more efficient or safer. As industries across the board, including technology manufacturers, seek to minimize their environmental footprint, chemicals like SMBS, when used responsibly, become essential tools in achieving these sustainability goals. Its role highlights the complex chemical solutions required to address the environmental challenges posed by industrialization.
Emerging Green Technologies
The development of green technologies often involves novel chemical processes. While not always directly branded as a “green” chemical, SMBS contributes to the infrastructure supporting these innovations. For example, in some experimental battery technologies or fuel cell designs, precise chemical control of redox reactions is critical. SMBS, as a well-understood reducing agent, could potentially find applications in these emerging fields, either in the synthesis of new electrode materials or in the electrolyte conditioning.
Similarly, in bioremediation efforts, where microbes are used to clean up pollutants, SMBS might be used to condition the environment or treat specific compounds that are resistant to biological degradation. As the field of sustainable chemistry advances, the properties of established compounds like SMBS are continually re-evaluated for their potential in new, environmentally friendly applications, thereby cementing its relevance in the ongoing technological revolution focused on planetary health.
Navigating Safety, Regulations, and Future Innovations
The widespread application of sodium metabisulfite across various tech-related sectors necessitates a rigorous focus on safety, regulatory compliance, and continuous innovation to optimize its use. Its benefits come with responsibilities, particularly regarding human health and environmental protection.
Compliance in Tech Production: Handling and Storage
Given its chemical nature, particularly its ability to release sulfur dioxide gas, the handling, storage, and transport of sodium metabisulfite are subject to strict industrial safety protocols and regulatory frameworks. For tech companies using SMBS in their manufacturing processes—whether for water treatment, material processing, or as an additive—adhering to these guidelines is not optional. This includes ensuring proper ventilation in work areas, providing appropriate personal protective equipment (PPE) for workers, and implementing secure storage solutions to prevent accidental release or exposure.
Compliance extends to documentation, including Safety Data Sheets (SDS), which provide comprehensive information on hazards, safe handling procedures, and emergency measures. The integration of digital safety management systems and advanced sensor technologies for environmental monitoring are becoming standard practice in tech-driven industries to ensure workplace safety and regulatory adherence, reflecting the broader technological approach to managing chemical use.
Health, Safety, and Environmental Impact
While SMBS is generally recognized as safe for specific applications when handled correctly, especially in very dilute forms (e.g., as a food preservative in minute quantities), its industrial use requires caution. Inhalation of high concentrations of sulfur dioxide gas, which SMBS releases, can cause respiratory irritation. Therefore, environmental control technologies, such as industrial air scrubbers and monitoring systems, are often deployed in facilities using large quantities of SMBS to protect both workers and the surrounding community.
From an environmental perspective, while SMBS is crucial for dechlorinating wastewater, excessive or uncontrolled discharge could potentially impact aquatic ecosystems. Responsible chemical management, therefore, includes careful dosing and post-treatment monitoring to ensure environmental impact is minimized. This balance between utility and environmental stewardship is a key challenge and a continuous area of innovation within the tech industry’s sustainability initiatives.

Research Horizons: Optimizing Tech Applications
The future of sodium metabisulfite in the tech sector lies in continued research and optimization. Scientists and engineers are constantly exploring ways to leverage its properties more efficiently, reduce its environmental footprint, and discover new applications. This includes developing more precise delivery systems to minimize waste, exploring alternative synthesis routes that are greener, and investigating its potential in novel material science contexts.
For instance, can SMBS contribute to the next generation of biodegradable plastics, or play a role in advanced recycling techniques for electronic waste? As nanotechnology and biotechnology continue to evolve, there may be unforeseen applications for SMBS at the micro and nano scales, where its reducing and stabilizing properties could be highly beneficial. The ongoing interplay between fundamental chemistry and applied technology ensures that even a seemingly simple compound like sodium metabisulfite will remain a relevant and evolving component of our technologically advanced world. Its story is a reminder that behind every grand technological leap, there are often humble chemical enablers making it all possible.
aViewFromTheCave is a participant in the Amazon Services LLC Associates Program, an affiliate advertising program designed to provide a means for sites to earn advertising fees by advertising and linking to Amazon.com. Amazon, the Amazon logo, AmazonSupply, and the AmazonSupply logo are trademarks of Amazon.com, Inc. or its affiliates. As an Amazon Associate we earn affiliate commissions from qualifying purchases.